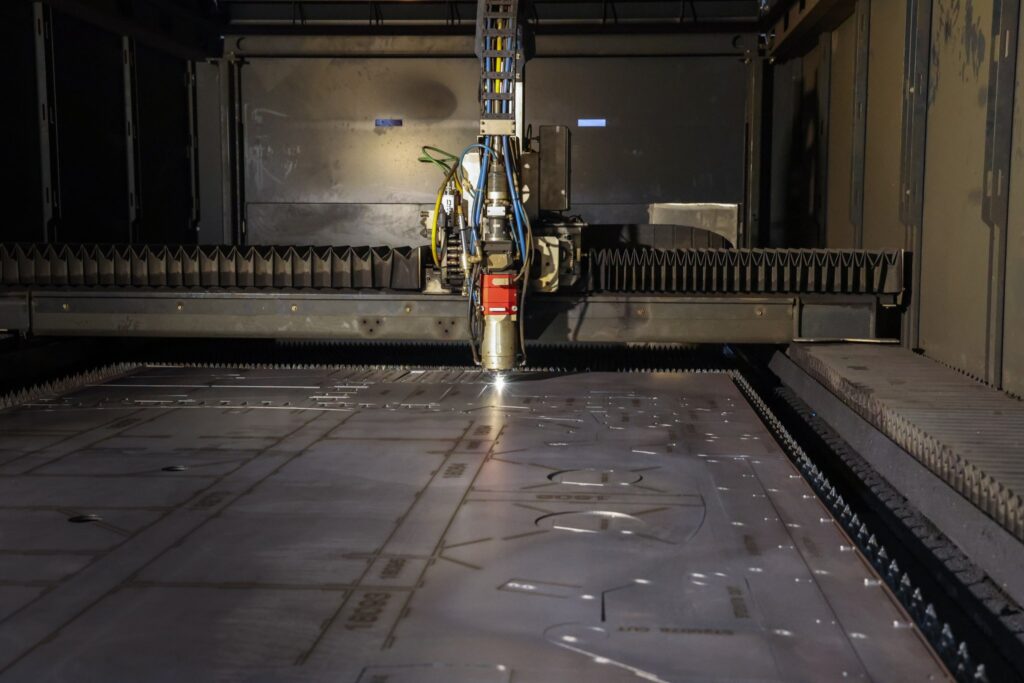
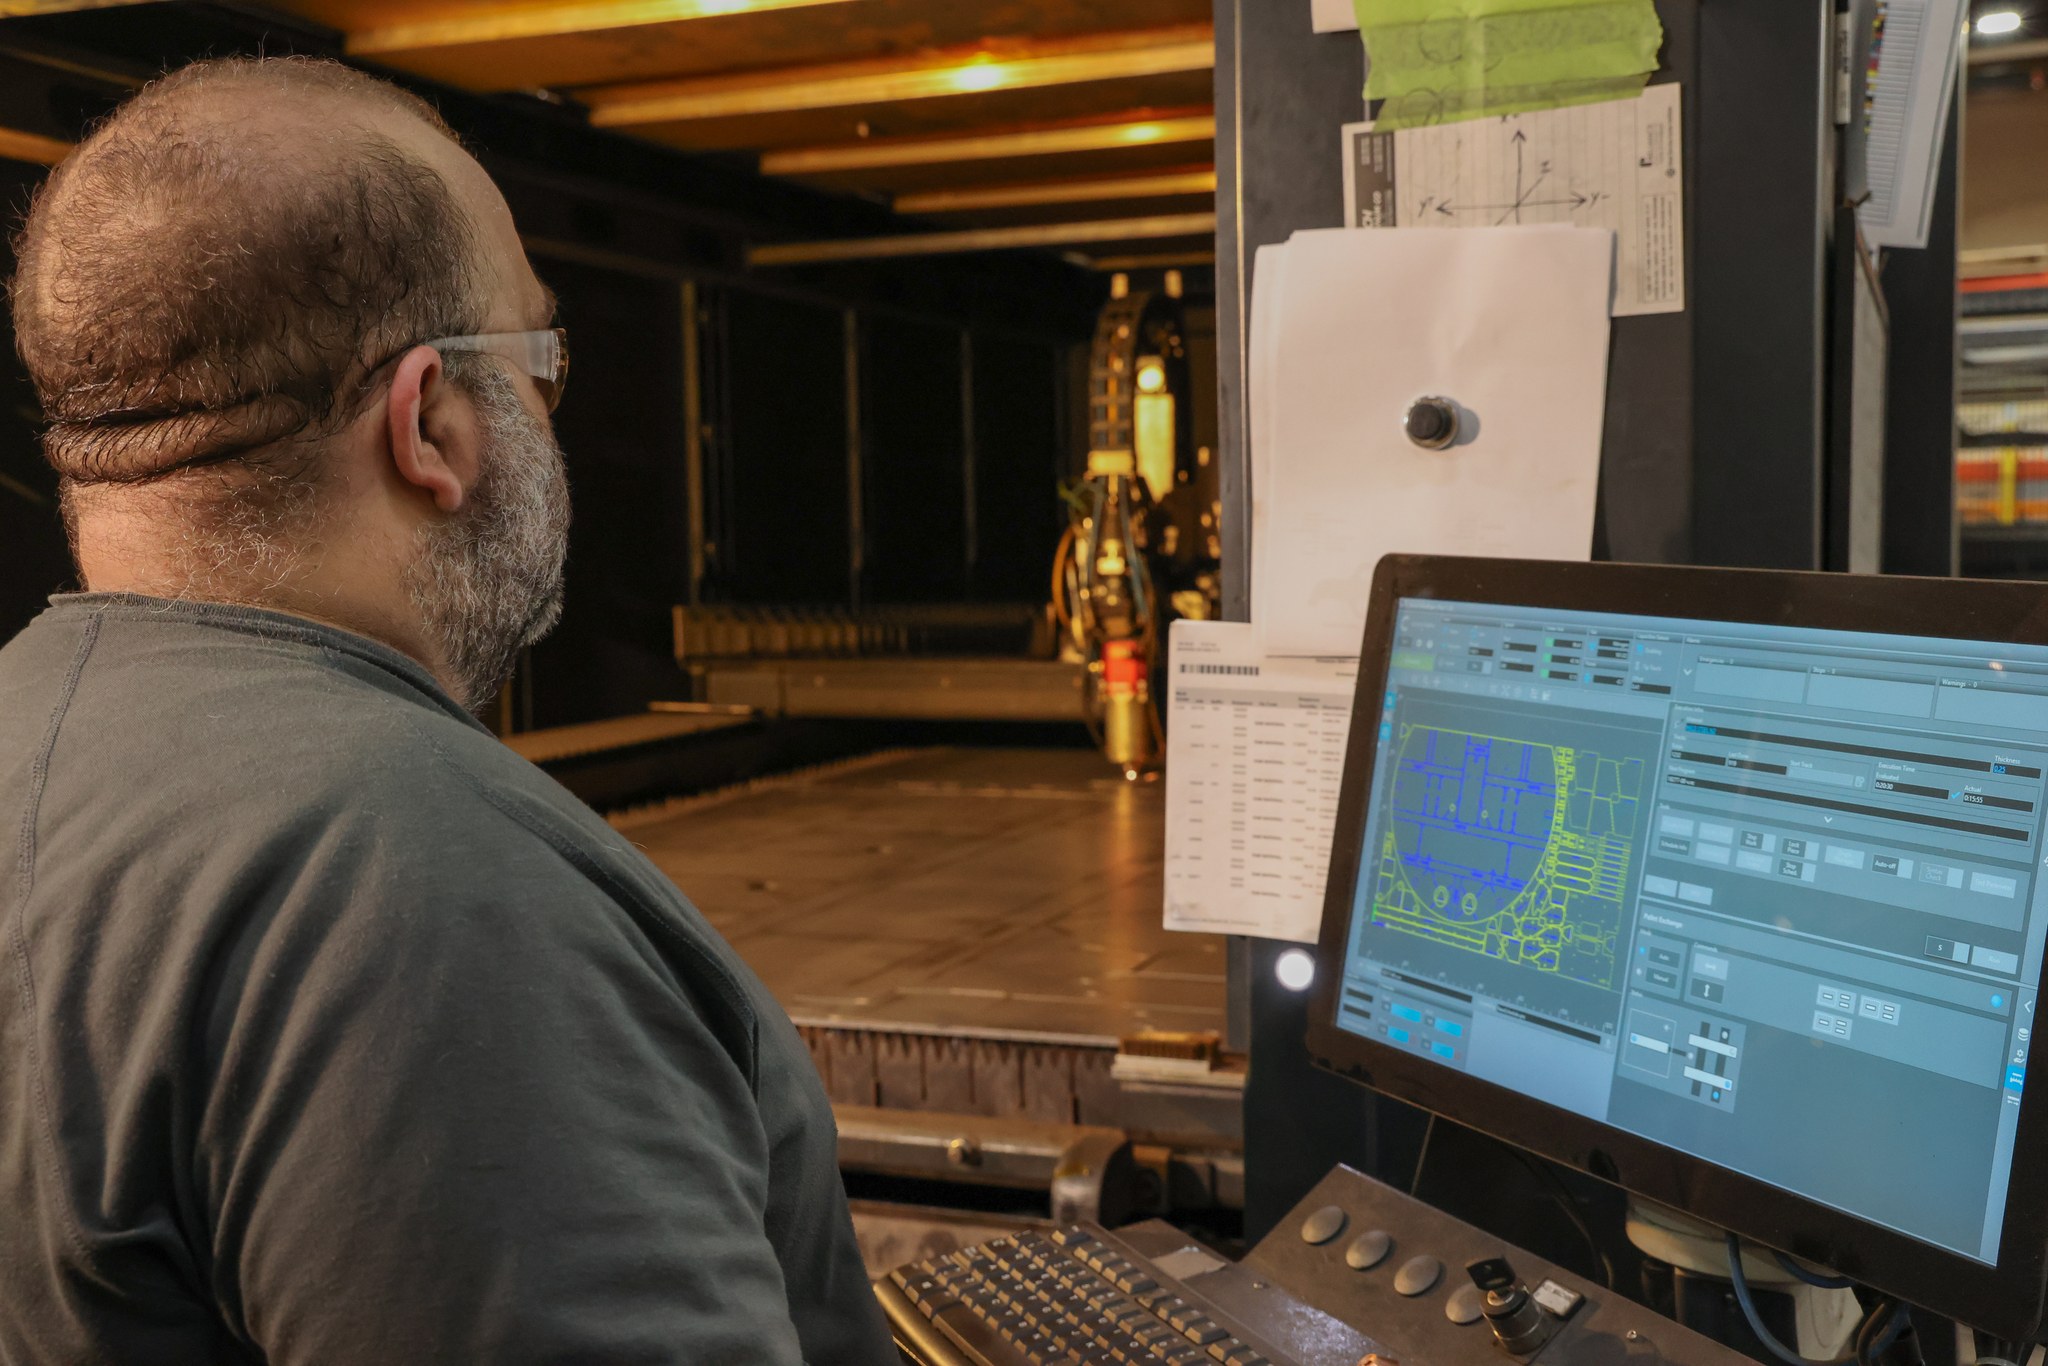
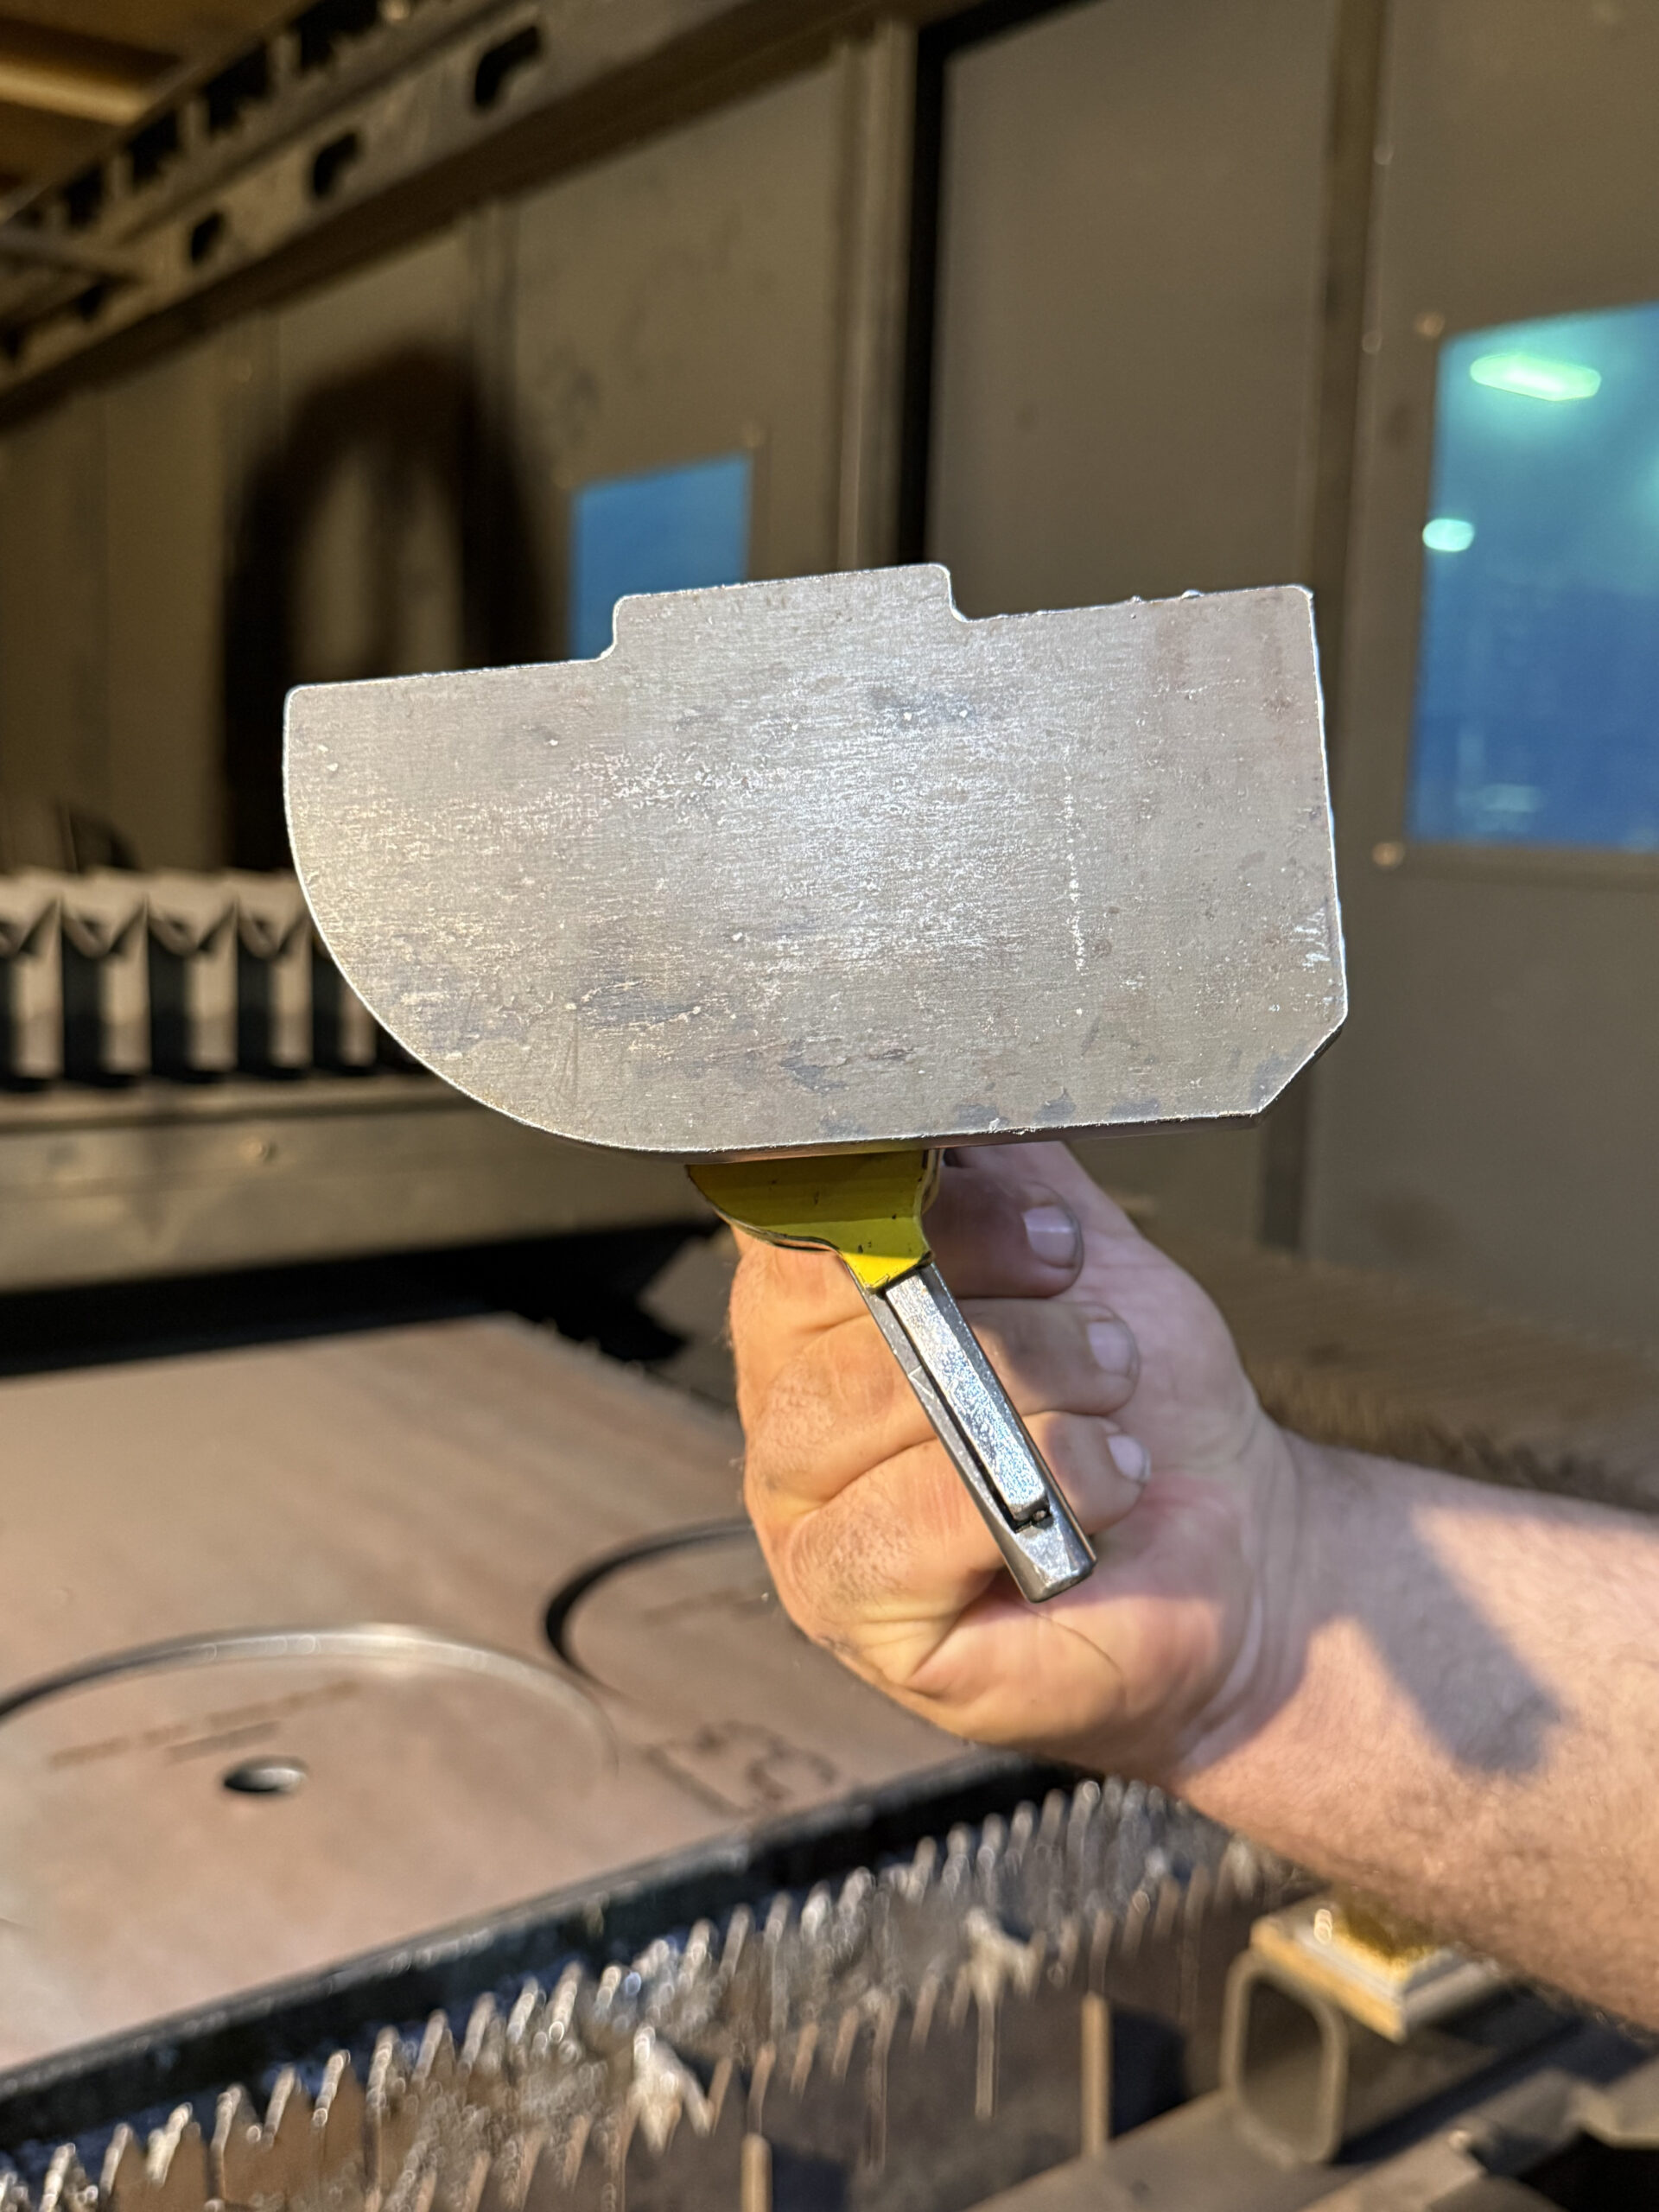
We provide high quality precision cuts using advanced laser technology and fiber laser cutting machines. Our laser cutting services deliver ultra-high-speed blanking, extreme edge quality, and heavy plate cutting. We cut carbon steel, stainless steel, aluminum, and more. With 20,000 watts of fiber laser power, 4.2G linear motor acceleration, dynamic assist gas controls, and automated 15-second dual pallet changers, we process sheet metal up to 13.3 by 6.7 feet with positioning repeatability of plus or minus 0.015 mm.
By pairing a 20 kW linear-drive cutter with a high-speed 6 kW and 10kW cell, Red Oak Fabrication handles both high-volume light gauge blanking and heavy industrial plate work. This gives you high precision and high speed on one shop floor.
| Specification | Cutlite Penta FAST 4020 | BySmart Fiber 3015 | BySmart 3015 |
|---|---|---|---|
| Laser resonator power Piercing speed and max plate thickness | 20,000 W (20 kW) IPG Photonics | 10,000 W (10 kW) fiber source | 6,000 W (6 kW) fiber source |
| Max working sheet bed Sheet stock size and nest yield | 13.3′ × 6.7′ | 10.0′ × 5.0′ | 10.0′ × 5.0′ |
| Drive motion system Acceleration between cuts | Linear motors with absolute encoders | Dual-motor rack-and-pinion, flying optics gantry | High-speed CNC axis drive |
| Max positioning speed Point-to-point travel between cuts | Exceeding 100 m/min | 140 m/min (5,511 IPM) | 140 m/min (5,511 IPM) |
| Cutting head Focal-point control across thickness | EVO 3 high-power autofocus | Autofocus (ByPos Fiber) | High-precision fiber optical head |
| Pallet exchange Load and unload without stopping the cut | 15-second dual-level shuttle | Dual-bed shuttle | Dual-bed shuttle |
| Machine accuracy Tolerance for automated downstream bending | ±0.03 mm · repeatability ±0.015 mm | ±0.10 mm · repeatability ±0.05 mm | ±0.10 mm · repeatability ±0.05 mm |
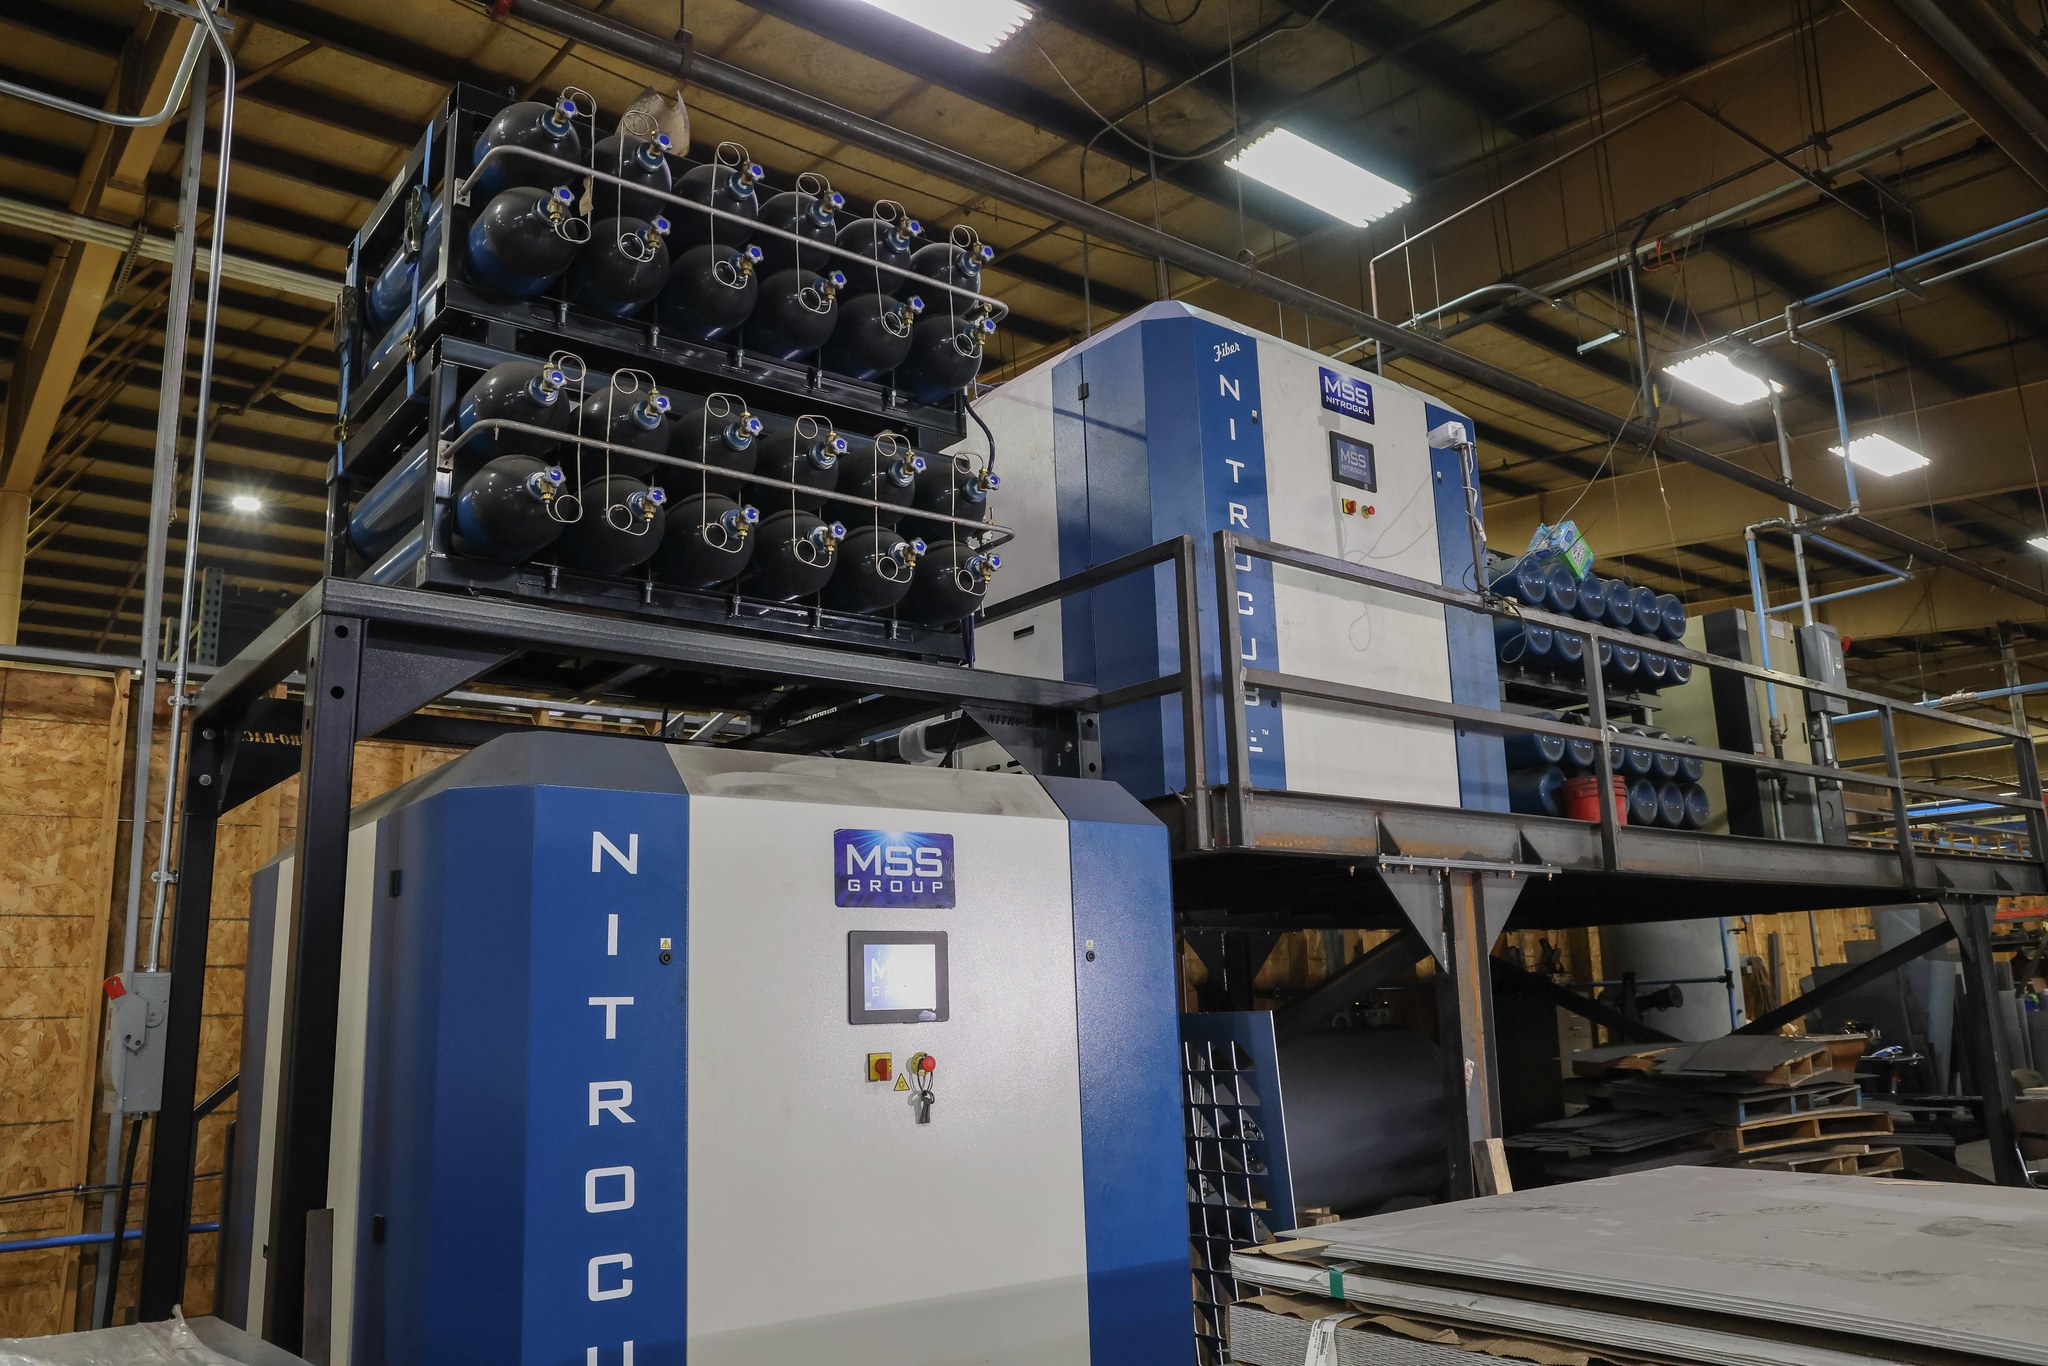
Our 20 kW, 6 kW fiber and 10kW lasers use dynamic fluid gas management. We use high-pressure nitrogen for oxide-free, weld-ready edges. We use oxygen for thick steel plate piercing. This lets us match the assist gas to each material for the best edge finish.
| Material Classification Grade / Alloy | Max Cutting Thickness | Edge Finish & Assist Gas Strategy |
|---|---|---|
| Carbon & Mild Steel A36, A572 Gr. 50, 1018 | Up to 2.0″ 50 mm | O2 exothermic cutting for heavy plate; high-pressure N2 for thin-gauge dross-free edges. |
| Stainless Steel 304, 304L, 316, 316L | Up to 1.18″ 30 mm | High-pressure N2 prevents surface oxidation for clean, weldable edges. |
| Aluminum Alloys 6061-T6, 5052-H32, 3003 | Up to 1.18″ 30 mm | High-speed nitrogen assist prevents burr formation and edge deformation. |
Fiber laser cutting at 20,000 watts requires elite machine dynamics. Only then can we use the full beam intensity without hurting part geometry. Three systems make this possible.
We track every Mill Test Report from intake through delivery. This proves the exact ASTM grade of each part.
We verify parts using calibrated coordinate measuring machines and precision height gauges.
Our certified welders adhere strictly to code standards and our fourth-generation family owners guide every metal fabrication line.
We work from four specialized facilities in Red Oak, Iowa. Together they provide comprehensive single-source metal fabrication. Laser-cut blanks move straight into our secondary departments, which include plasma cutting, CNC milling & tapping, robotic & manual welding, and blasting & powder coating.
Jim runs our laser floor and the drafting team behind it, so a fiber-cut part goes to the person who runs the lasers.
We reply in 1 business day. We deliver turnkey in 4–6 weeks from PO. Send us your print — we’ll take it from there.
We reply in 1 day & deliver turnkey in 4–6 weeks from PO.